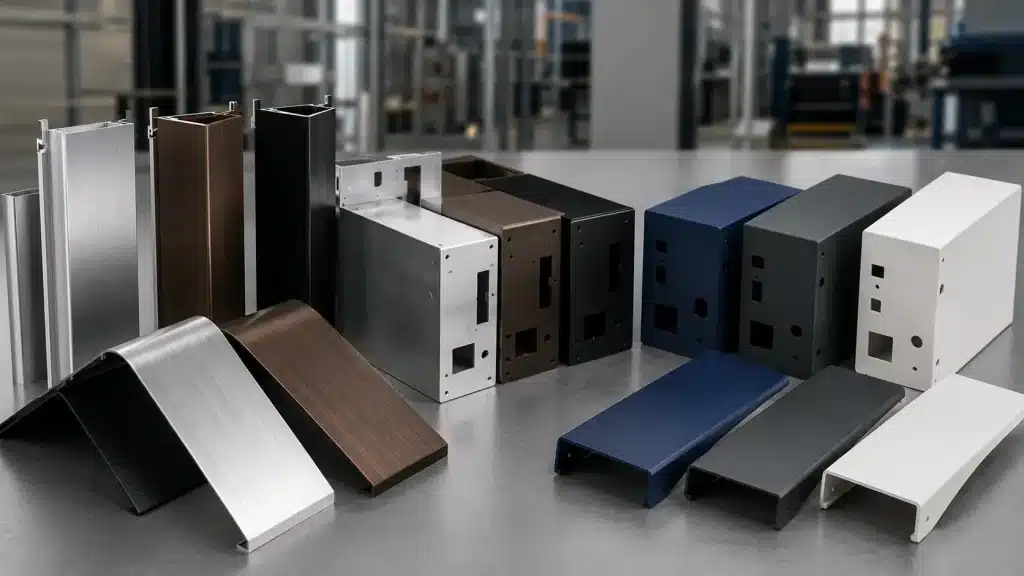
Anodizing vs Powder Coating Aluminum: Durability, Appearance and Cost
Anodizing and powder coating are two of the most common finishes for aluminum, but they protect and decorate the metal in fundamentally different ways. Anodizing converts the aluminum surface into a controlled oxide layer that remains integral with the substrate. Powder coating applies a separate polymer film that is melted and cured over a prepared surface.
That difference affects color, scratch behavior, edge coverage, UV stability, masking and dimensional control. Buyers comparing aluminum coating services should define the required outcome instead of asking only for “black,” “silver” or “outdoor quality.” Alloy, exposure, geometry, production volume and approved appearance all influence the correct route.
How the Two Finishes Are Created
Anodized coating is produced electrochemically. After cleaning and etching or brightening, the aluminum becomes the anode in an electrolyte. The process grows a porous aluminum-oxide structure partly into and partly above the original surface. The pores may be dyed, then sealed to improve durability and stabilize the finish.
Electrostatic powder coating sprays charged thermoset powder onto a grounded, pretreated component. Oven heat melts, flows and cures the powder into a continuous film. The pretreatment, film thickness and cure schedule are as important as the powder chemistry itself. A premium powder over poor preparation is still a poor coating system.
Anodizing vs Powder Coating: At-a-Glance
Decision factor | Anodizing | Powder coating | Design implication |
|---|---|---|---|
Finish type | Integral aluminum oxide | Separate cured polymer film | Failure and repair modes differ |
Visual character | Metallic; substrate texture remains visible | Opaque color, smooth or textured | Choose by intended design language |
Color range | Limited and alloy-sensitive | Very broad standard and custom range | Samples should use production material |
Typical build | Thin relative to powder | Higher film build | Fits, threads and sharp details need review |
Wear behavior | Hard surface; can show base-metal damage | Tough film; may chip or scratch through | Match damage type to service |
UV exposure | Natural tones generally stable; dyes vary | Exterior powders can be highly UV stable | Specify chemistry and warranty class |
Edges and recesses | Treatment follows accessible aluminum surface | Faraday areas and edges need process control | Geometry influences coverage |
Repair | Difficult to blend invisibly | Liquid touch-up possible but may show | Plan lifecycle repair before approval |
Economic fit | Consistent alloy, color and bath-compatible parts | Repeat batches, broad color and oven-compatible parts | Compare complete production route |

1. Durability Starts with the Service Environment
The word “durable” is incomplete without a failure mode. A handrail may need resistance to abrasion and skin oils. A facade needs long-term color and gloss retention under ultraviolet exposure. A machine cover may face impact, cleaning chemicals and repeated handling. Coastal equipment adds chloride exposure and water retention. The finish must be matched to the real environment rather than ranked with one generic score.
Anodizing produces a hard mineral surface that resists abrasion and cannot peel like a separate film. If severe impact penetrates the oxide, however, the damaged area can expose raw aluminum and is difficult to repair invisibly. Powder coating can create a tough, resilient barrier with good edge coverage, but deep scratches or chips may allow underfilm corrosion if pretreatment and maintenance are inadequate.
2. Corrosion Protection Is a System Property
Aluminum naturally forms a thin oxide film. Anodizing deliberately thickens and controls that oxide, while sealing reduces pore activity. Performance depends on alloy, anodic class, thickness, sealing quality, exposure and fabrication details. Powder coating relies on cleaning and conversion pretreatment for adhesion and corrosion resistance; film chemistry and cure then complete the system.
Neither finish corrects water traps, unsealed joints or incompatible fasteners. Cut edges, drainage holes, crevices and bimetallic contact should be reviewed during design. Accelerated salt-spray hours are useful only with a defined test method, specimen preparation and failure criterion; they do not translate directly into years of outdoor life.
3. Appearance: Metallic Depth vs Opaque Color
Anodizing preserves the visual character of aluminum. Brushed lines, extrusion flow marks, machining patterns, weld zones and alloy variation can remain visible. This can create a premium metallic finish, but it also means incoming material and fabrication must be visually consistent. Clear, bronze and black are common; dyed colors can vary with alloy, oxide thickness, bath control and sealing.
Powder coating hides more substrate color and offers a far wider palette of gloss levels, textures and special effects. Texture can reduce the visibility of minor handling marks, yet it should not be used to excuse dents, heavy scratches, weld spatter or poor grinding. Metallic powders may show orientation differences between parts, angles or application batches.
Sample rule: approve a production-representative coupon or first article made from the actual alloy, temper and surface preparation. A catalog chip cannot predict anodized batch variation, powder texture, gloss, metallic orientation or the visibility of welds and machining marks.
4. Alloy, Welding and Fabrication Affect the Result
Anodizing is especially sensitive to alloy chemistry and metallurgical history. Different aluminum grades—or even extrusions from different lots—may anodize to noticeably different tones. Weld metal and heat-affected areas can remain visible. Cast alloys may appear gray or mottled because of silicon and other constituents. The supplier should confirm alloy compatibility before a cosmetic finish is promised.
Upstream sheet metal laser cutting and bending operations affect both finish routes. Sharp burrs, oxide, heavy tool marks and poor weld cleanup remain quality risks. Early engineering and DFM support can define cosmetic faces, grain direction, hanging points, drainage, masking and acceptable contact marks.
5. Thickness, Tolerances and Masking
Anodizing changes dimensions because part of the oxide grows above the original surface. The exact dimensional effect depends on the specified process and thickness. Powder coating creates a substantially thicker film and can bridge fine details or interfere with threads, holes, bearing seats, electrical contacts and assembly fits. Drawings should identify coating-free zones and pre-finish dimensions.
Interface | Anodizing consideration | Powder-coating consideration |
|---|---|---|
Threads | Allowance or masking may be needed | Usually mask or chase where fit is critical |
Bearing and seal seats | Define post-finish size and measurement | Mask to avoid excessive film buildup |
Electrical bonding | Remove or mask at contact zone | Mask dedicated grounding/contact surfaces |
Sharp edges | Finish follows the edge; handling damage matters | Film may thin or pull away at very sharp edges |
Deep recesses | Bath access and rinsing/drainage are critical | Faraday-cage effect can reduce deposition |
Hanging points | Electrical contact marks must be located | Rack hooks can leave uncoated witness marks |

6. Outdoor Color and UV Stability
Clear and architectural bronze anodizing are widely used outdoors because the metallic finish can weather predictably when properly specified and sealed. Organic dyes vary in lightfastness, so a vivid indoor anodized color should not automatically be accepted for exterior service. Color limits and approved viewing conditions are important because anodized aluminum naturally shows more variation than an opaque paint film.
Powder coating can provide strong exterior color and gloss retention when the correct resin class is selected. Polyester architectural powders are common, but product classes and warranties differ. A low-cost general-purpose powder should not be assumed equivalent to a system qualified for severe UV or coastal exposure. Color, gloss, pretreatment and cure records all belong in the specification.
7. Cost Depends on Batch, Color and Process Route
Anodizing cost is influenced by alloy, finish preparation, thickness, color, sealing, bath size, racking and rejection risk. Cosmetic requirements can be expensive when batches must be tightly color-matched or when welds and surface defects require extra preparation. Powder-coating cost includes cleaning and pretreatment, masking, racking, color change, application, oven curing, inspection and packaging.
Cost driver | May favor anodizing | May favor powder coating |
|---|---|---|
Appearance target | Natural metallic character | Opaque standard color or texture |
Material consistency | Same alloy and lot are controlled | Mixed visual substrate can be hidden |
Color program | Stable clear/bronze/black family | Broad recurring RAL or custom palette |
Tolerance need | Thin integral finish is advantageous | Masking is acceptable in the route |
Part envelope | Fits available anodizing bath | Fits booth, rack and cure oven |
Repair strategy | Replacement/re-anodizing is acceptable | Local liquid touch-up is acceptable |
The lowest quoted price may not be the lowest total cost. Add preparation, masking, inspection, rework, batch matching, packing and transport. Also consider whether a supplier can coordinate fabrication and finishing without damage or repeated handling.
Selection Checklist
Question | Anodizing may fit when | Powder coating may fit when |
|---|---|---|
Visual intent | Metal should remain visibly metallic | Opaque color or texture is desired |
Wear mode | Hard abrasion-resistant surface is valuable | Impact-resilient polymer film is valuable |
Color range | Limited controlled tones are acceptable | Broad color selection is essential |
UV exposure | Qualified natural/architectural anodizing | Qualified exterior powder system |
Substrate variation | Alloy and finish history are consistent | Coverage should hide visual variation |
Dimensions | Thin finish helps critical interfaces | Masking and film allowance are practical |
Geometry | Bath access and drainage are sound | Electrostatic access and oven cure are sound |
Repair | Invisible field repair is not expected | Touch-up procedure can be accepted |
Economics | Bath-compatible repeat parts and few colors | Repeat batches and stable color programs |
What to Include in an Aluminum Finishing RFQ
- Part data: drawing revision, alloy and temper, dimensions, weight, weld condition and annual quantities.
- Finish system: anodizing class/type/thickness/color/seal or powder chemistry, pretreatment and film-thickness range.
- Service environment: indoor or outdoor use, UV, coastal salts, humidity, cleaners, temperature and abrasion.
- Appearance: visible faces, color reference, gloss, texture, grain direction, approved sample and allowable variation.
- Masking and interfaces: threads, bores, datums, contacts, bearing seats, seal areas and permissible rack marks.
- Validation: first article, thickness measurement, adhesion or sealing checks, corrosion test and certificates.
- Commercial scope: batch size, color changes, packaging, touch-up method, spare parts and delivery sequence.
Frequently Asked Questions
Is anodizing more durable than powder coating?
Not in every service condition. Anodizing provides a hard integral surface, while powder creates a tough polymer barrier. The better finish depends on abrasion, impact, UV, chemicals and repair expectations.
Which finish is better for outdoor aluminum?
Both can perform well when correctly specified. Architectural anodizing and qualified exterior powder systems are common; alloy, color, pretreatment, thickness, climate and maintenance determine suitability.
Can anodized aluminum be color matched perfectly?
Exact matching is difficult because alloy, temper, surface preparation, oxide thickness and batch conditions affect color. Agree on an acceptable range using production material.
Can powder coating hide aluminum defects?
It can hide some color variation, especially with texture, but it cannot reliably conceal dents, deep scratches, weld distortion or contamination. Substrate quality still matters.
Can both finishes be repaired in the field?
Powder can often be touched up with a compatible liquid coating, although the patch may show. Local anodizing repairs rarely match the surrounding finish and replacement may be preferable.
Validate the Finish Before Full Production
Use a production-representative first article with the actual alloy, extrusion or sheet lot, welding, machining, grain direction and masking details. Inspect color, gloss, texture, film or oxide thickness, sealing or cure, contact marks, coverage and assembly fit. Review the sample under agreed lighting and at an agreed viewing distance. Do not approve a hand-prepared showroom coupon as proof of a repeatable production route.
A coordinated custom metal manufacturing route can align fabrication, surface preparation, finishing and packaging. Nova’s quality and project approach can support first-article approval and finish documentation according to the component’s risk and end use.