The Imperative for Perfection in Power Transmission
In the world of mechanical engineering, gears are the heart of power transmission. They are the components responsible for transferring motion and torque reliably, efficiently, and often, at high speeds and under extreme loads. Whether in an aerospace actuator, a precision industrial gearbox, or a high-performance vehicle drivetrain, the requirement for a gear’s tooth profile to be flawless is absolute.
Initial gear production—through processes like hobbing or milling—is accurate, but not perfect. The materials used in high-performance gears (typically alloy steels) must undergo heat treatment to achieve the necessary core strength and surface hardness. This crucial hardening process, however, causes inevitable thermal distortion and dimensional deformation in the gear’s geometry.
This is the moment when Grinding Service steps in. Grinding is not just a finishing step; it is a specialized, high-precision machining process used to correct these heat-treatment distortions, remove material down to the micron level, and ensure the gear meets its demanding performance class. This article delves into the necessity of gear grinding, the technology behind it, and why it is the key to achieving micron-level precision for high-performance Gear Fabrication.
The Necessity of Grinding in the Gear Manufacturing Workflow
The path of a high-performance gear from raw material to a finished product is complex, and grinding is positioned as the final, most critical stage, differentiating a standard gear from a precision component.
1.1. Correcting Thermal Distortion: The Primary Goal
The primary reason for gear grinding is to compensate for the volumetric and geometric changes caused by heat treatment (such as carburizing, carbon-nitriding, or induction hardening). While hardening makes the gear durable, it warps the gear tooth profile, alters the pitch, and affects the tooth alignment. Without grinding, these imperfections would lead to:
- Excessive Noise and Vibration (NVH): Misalignment causes uneven contact between mating teeth.
- Reduced Efficiency: Friction increases significantly due to imperfect contact surfaces.
- Premature Wear and Failure: Stress concentrations occur at distorted points, drastically shortening the gear’s lifespan.
Grinding meticulously removes the minimal material necessary to restore the specified profile, lead, and pitch accuracy, often achieving quality classes as tight as DIN 3 to DIN 5 (ISO equivalent standards), which is vital for high-speed applications.
1.2. The Quest for Superior Surface Finish
Grinding inherently produces a far smoother surface finish than initial cutting processes (hobbing or shaping). A smoother tooth flank results in:
- Reduced Friction: Lower energy losses and higher operational efficiency (especially critical in electric vehicles).
- Increased Lubrication Efficacy: Smoother surfaces retain the lubricant film better, further minimizing metal-to-metal contact.
- Quieter Operation: The reduction in roughness eliminates micro-vibrations, leading to extremely low noise (NVH) levels.

Types of Precision Gear Grinding Technologies
Modern Grinding Service employs highly sophisticated CNC machines utilizing different methods, each tailored to specific gear types and precision requirements. These methods fall into two main categories: Form Grinding and Generating Grinding.
2.1. Gear Generating Grinding (Continuous Process)
Generating grinding is highly suitable for high-volume production due to its efficiency and speed.
- Principle: This method uses a grinding wheel (often a threaded wheel, known as a ‘grinding worm’) that is constantly rotating while in mesh with the gear workpiece, which also rotates on its axis. The gear profile is generated through the continuous rolling motion between the wheel and the workpiece, akin to the action of hobbing.
- Advantages: This continuous action is exceptionally fast and repeatable, making it cost-effective for medium to large production runs of standard spur and helical gears.
- Limitation: It has limitations in applying complex tooth root or tip modifications that may be required for noise optimization.
2.2. Gear Profile Grinding (Form Grinding)
Profile grinding is the pinnacle of precision, offering the highest control over the tooth geometry.
- Principle: This method uses a single grinding wheel that is precisely dressed to the exact profile of a single gear tooth space. The wheel runs between two opposing teeth, grinding both surfaces simultaneously. The CNC machine moves the wheel precisely along the theoretical involute curve, tooth by tooth.
- Advantages: This discrete, tooth-by-tooth process allows for virtually any desired profile modification. Engineers can apply specific profile corrections (crowning, tip relief, root relief) to optimize the gear’s performance under load, minimize noise, and achieve the tightest tolerances, often reaching DIN 3 or DIN 4
- Application: Primarily used for large gears, prototype runs, and critical aerospace or high-speed motorsport applications where absolute profile accuracy is paramount.
2.3. Specialized Grinding Methods
For complex gear geometries, further specialized grinding techniques are employed:
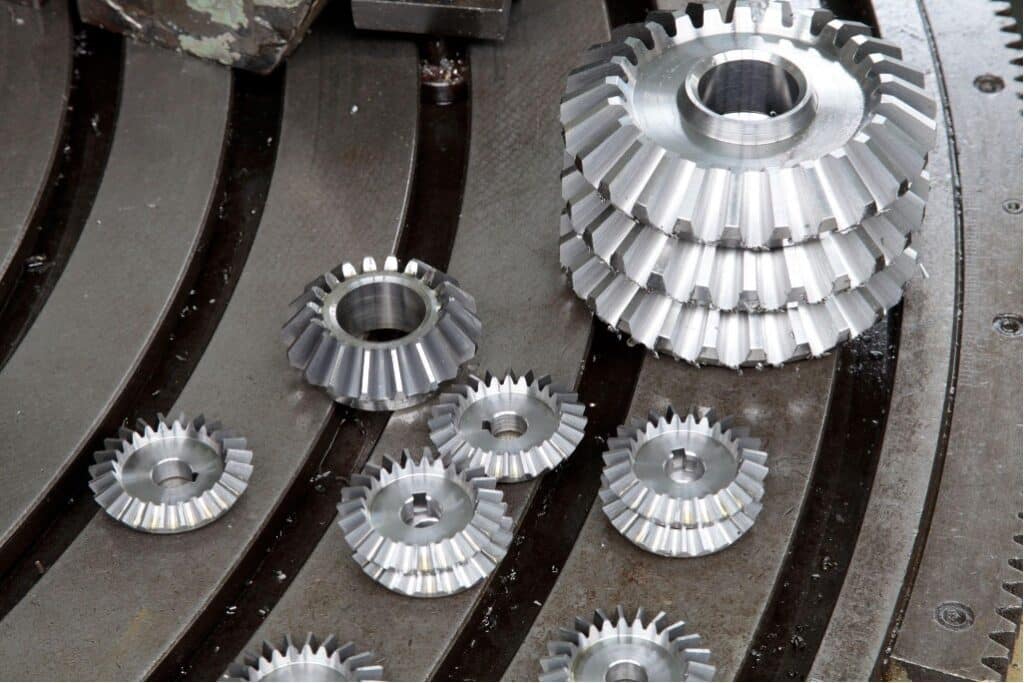
- Bevel Gear Grinding: Utilizes cup wheels to finish the complex conical shape of straight, spiral, or hypoid bevel gears, which are commonly found in differentials.
- Worm Gear Grinding: Requires highly specialized grinding machines to maintain the precise helix angle and tooth profile of the worm mechanism.
The Micron-Level Difference: Understanding Tolerances in Gear Grinding
In engineering, “precision” is a relative term. While the tolerances achieved with a standard CNC Milling Service (e.g., +/- 0.05 mm) are sufficient for many applications, in the world of high-performance Gear Fabrication, these tolerances are unacceptably loose. Here, we are talking about precision at the micron level (1 micron = 0.001 mm).
3.1. Gear Quality Standards (DIN and AGMA)
Gear quality is defined by international standards (such as DIN 3961/3962 or AGMA 2000/2015). These standards are based on a series of parameters that measure how much a gear deviates from its theoretical perfection. The quality class is expressed as a number, typically ranging from 1 (highest precision) to 12 (coarsest) in the DIN standard.
A gear produced only by milling or hobbing, without heat treatment, is typically a DIN 7-9 quality. However, the distortions that occur after heat treatment (hardening) can degrade this quality down to a DIN 10-12 level. In contrast, a gearbox that must operate at high speed and with low noise usually requires a quality class between DIN 3 and DIN 5.
The only way to achieve this quality class is through a Grinding Service.
3.2. Critical Geometric Errors Corrected by Grinding
Grinding corrects specific errors that directly impact a gear’s performance:
- Profile Error ($f_{Hα}$): This is the deviation from the ideal curved profile of the tooth, known as the “involute.” This error prevents the gears from “rolling” smoothly against each other and causes noise. Grinding redraws this profile with micron-level accuracy.
- Helix Angle Error ($f_{Hβ}$): In helical gears, this is the deviation of the tooth’s angle from the theoretical helix line. This error causes the load to be unevenly distributed across the tooth face, leading to stress concentration on one edge. Grinding perfects this angle along the entire tooth width.
- Pitch Deviation ($f_p$): This is the inconsistency in the distance between adjacent teeth. During heat treatment, some teeth move closer together while others move farther apart. This creates shock loads and “rattle” during torque transmission. Grinding precisely equalizes the distance between every tooth.

The Role of Material and Its Challenges in the Grinding Process
The complexity of a grinding service stems not only from its geometric precision but also from the properties of the materials it works with.
4.1. Grindability and Material Hardness
High-performance gears must withstand extreme loads and wear. For this reason, they are typically manufactured from alloy steels such as 8620, 4140, 9310, or nitriding steels. During the Gear Fabrication process, these parts undergo heat treatments (usually carburizing or induction hardening) that bring their surface hardness up to 58-64 HRC (Rockwell C).
At this level of hardness, the material can no longer be machined with conventional cutting tools (like milling cutters or lathe tools). The only thing that can shape the material is abrasive grains that are even harder. This is where the Grinding Service comes in.
4.2. The Risk of “Grinding Burn”
Grinding is, in essence, a high-speed friction process that generates an immense amount of heat. The greatest risk in the grinding process is thermal damage known as “grinding burn.” If the process is not properly controlled, the localized temperature increase on the gear’s surface will ruin the material’s microstructure:
- Re-tempering (Softening): If the surface gets too hot, the hardened structure is “tempered” back and becomes soft. This catastrophically reduces the gear’s wear resistance.
- Re-hardening (Cracks): If extreme heat is followed by a sudden quench (by the coolant), an undesirable, highly brittle “martensite” layer forms on the surface. This layer leads to microscopic cracks and can cause the gear to fail catastrophically during operation.
4.3. How to Prevent Grinding Burn (The Secret of a High-Quality Service)
An expert Grinding Service provider, like Nova Fabrication, controls three key variables to manage this risk:
- Correct Wheel Selection: A wheel is chosen that matches not only the material’s hardness but also its “grindability.” Different abrasives like Aluminum Oxide, CBN (Cubic Boron Nitride), and different bond hardnesses are used.
- Precise Feed Rate: The machine is set to remove only a few microns of material at a time. These “spark-out” passes minimize heat generation.
- Coolant Management: The role of the coolant is not just to cool. It also cleans metal chips (swarf) from the wheel’s pores with high pressure, keeping the wheel “sharp.” A clogged wheel will “rub” instead of “cut,” causing an immediate burn.
Beyond the Teeth: The Importance of All Gear Surfaces
The secret to a high-performance gear does not lie only in its perfect tooth profiles. All other critical surfaces of the gear, such as those that sit on the shaft or in a bearing, must also have the same micron-level precision. Otherwise, even perfect gears will be misaligned and fail.
5.1. ID/OD Cylindrical Grinding
A gear’s performance depends on how concentric its tooth profile (pitch circle) is with the central axis of the bore.
- First Step (Turning): The part is first machined on a Cnc Turning Service. At this stage, a small amount of “stock” is left on for heat treatment and grinding.
- Heat Treatment: As the part hardens, the inner bore (ID) and outer diameters (OD) also distort.
- Final Step (Grinding): The Grinding Service then grinds the gear’s inner bore (ID) and, if applicable, its shaft diameter (OD). This process ensures the gear fits onto its bearings or shaft with zero play (zero runout). If there is an eccentricity error between the bore and the tooth profile, the gear will “wobble” as it rotates, causing vibration throughout the entire system.
5.2. Surface Grinding
Helical gears, in particular, create an axial “thrust” force as they rotate. This force is countered by the gear’s side faces.
- Surface Grinding ensures that these side faces (faces) are perfectly flat and perfectly perpendicular to the axis of the bore.
- If these faces are not properly ground, the gear will “wobble” laterally as it rotates, which applies an uneven load to the bearings and other components.