CNC Punching vs Laser Cutting: Which Process Is More Cost-Effective?
CNC punching and laser cutting are both widely used to manufacture sheet metal components. Although the two processes can produce similar parts, their cost structures are different.
CNC punching is often economical for repetitive hole patterns, standard geometries and medium-to-high production volumes. Laser cutting generally provides greater flexibility for complex contours, prototypes and frequently changing designs.
The most cost-effective choice depends on part geometry, material thickness, production volume, tooling requirements and downstream operations—not simply the machine’s hourly rate.
How Does CNC Punching Work?
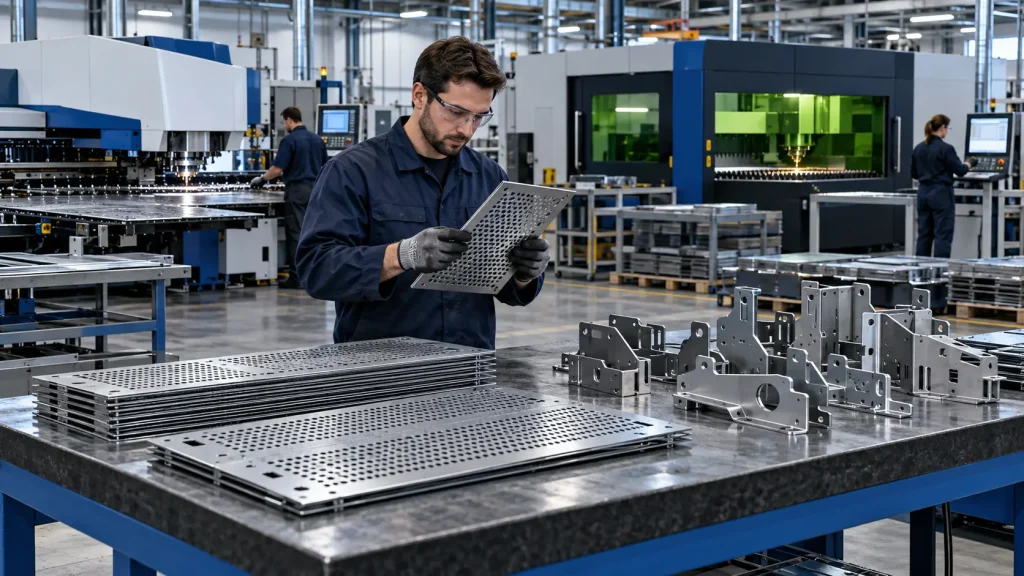
CNC punching uses a punch and die set to apply mechanical force to sheet metal. The machine positions the sheet and repeatedly creates holes, slots, ventilation patterns and formed features.
Nova Fabrication’s CNC punch cutting service can be used for parts requiring repetitive features and efficient sheet processing.
Punching is particularly effective for:
- Repeated round or rectangular holes
- Ventilation and perforation patterns
- Electrical cabinets
- Equipment panels
- Metal shelving
- Brackets and mounting plates
- Medium and high-volume production
In addition to cutting, suitable tooling may create forms such as louvers, knockouts, countersinks and small embossments. Combining cutting and forming in one setup can reduce secondary operations.
How Does Laser Cutting Work?
Laser cutting uses a focused beam to melt or vaporize material along a programmed path. An assist gas removes molten material and helps control edge quality.
Unlike punching, sheet metal laser cutting does not require a physical tool for every feature. This makes it highly flexible for prototypes, complex shapes and design revisions.
Laser cutting is commonly preferred for:
- Complex external contours
- Irregular holes and slots
- Small production batches
- Prototype parts
- Frequent design changes
- Components with many different geometries
- Projects where tooling investment is undesirable

CNC Punching vs Laser Cutting at a Glance
Factor | CNC Punching | Laser Cutting |
Initial tooling | May require dedicated tooling | Usually no dedicated cutting tool |
Repetitive holes | Very efficient | Efficient, but may be slower for dense patterns |
Complex contours | Limited by tool geometry | Highly flexible |
Design changes | May require new tooling | Usually handled through programming |
Formed features | Can produce louvers and knockouts | Requires a separate forming process |
Edge marks | Possible tool marks and burr | Heat-affected edge and possible dross |
Best production range | Medium to high volume | Prototype to high volume |
Typical cost advantage | Repeated standard features | Complex or frequently changing parts |
When Is CNC Punching More Cost-Effective?
CNC punching usually becomes more economical when the same standard features are repeated many times.
For example, a cabinet panel may contain dozens of identical ventilation holes. Once the correct punch tool is installed, each stroke can be completed quickly. The cost per feature can therefore become lower as order volume increases.
Punching may offer a cost advantage when:
- The part contains many repeated holes
- Standard tools are already available
- Production quantities are stable
- Sheet thickness is suitable for punching
- Parts require louvers or knockouts
- Minor tool witness marks are acceptable
However, special tooling introduces an upfront cost. If only a small number of parts are required, the tooling investment may outweigh the faster production cycle.
Tool wear, maintenance and setup time should also be included in the cost comparison.
When Is Laser Cutting More Cost-Effective?
Laser cutting is generally more economical when flexibility is more valuable than maximum punching speed.
A laser can move directly from one programmed geometry to another without installing a dedicated punch for each feature. This reduces tooling dependency and makes engineering changes easier to manage.
Laser cutting often provides better value when:
- Quantities are low or uncertain
- Several part variants are required
- External contours are complex
- Hole shapes are non-standard
- Design revisions are expected
- Prototype parts are needed quickly
- Tooling costs must be avoided
Good nesting can also place different components on the same sheet, improving material utilization across mixed-part orders.
For projects involving critical edge or dimensional requirements, the effects of kerf, burr, assist gas and heat input should be reviewed. These factors are explained in Nova’s guide to laser cutting tolerances and edge quality.

How Does Order Volume Affect the Decision?
Production volume is important, but there is no universal quantity at which punching automatically becomes cheaper than laser cutting.
The break-even point depends on:
- Number of holes per part
- Complexity of the external contour
- Available punch tools
- Cost of special tooling
- Material type and thickness
- Machine setup time
- Laser cutting speed
- Required secondary operations
- Expected future design revisions
For a simple panel with hundreds of identical holes, punching may become economical even at a moderate quantity. For a complicated component with many unique contours, laser cutting may remain competitive at much higher volumes.
This is why suppliers should evaluate the actual CAD data rather than make a decision based only on annual quantity.
Material Thickness and Geometry
Both processes can handle a range of sheet metals, including carbon steel, stainless steel and aluminium. Their practical limits depend on machine capacity, material properties and required quality.
Punching applies physical force to the sheet. Small holes in thick material may require high force and can increase tool wear or distortion risk.
Laser cutting does not mechanically contact the sheet, but thicker materials may require slower cutting speeds, higher laser power and more assist gas.
The relationship between hole size, sheet thickness and edge requirements should therefore be considered during design. Nova’s DFM guide for sheet metal parts explains how early design decisions can reduce manufacturing cost and lead time.
Do Not Compare Cutting Cost Alone
The lowest cutting price does not always create the lowest finished-part cost.
The full process may include:
- Deburring
- Countersinking
- Tapping
- Forming
- Bending
- Welding
- Grinding
- Powder coating
- Inspection
- Assembly
Punching may be advantageous if louvers or knockouts can be created during the same machine cycle. Laser cutting may be preferable if it reduces tooling, programming complications or design-change costs.
Nova Fabrication’s wider precision metal cutting services allow the cutting method to be evaluated as part of the complete manufacturing route.
Can Punching and Laser Cutting Be Used Together?
Yes. Some projects benefit from using both processes.
Punching may create repetitive holes and formed features, while laser cutting produces complex external profiles or special openings. The best manufacturing route may also change between prototype and serial production.
For example, prototypes may initially be laser cut to avoid tooling investment. After the design is validated and volumes increase, selected features may be transferred to punching.
Early engineering support can help determine whether one process or a combined route provides the best balance of cost, quality and lead time.
RFQ Checklist
To receive a reliable process comparison, include:
- 2D drawing and 3D model
- Material grade
- Sheet thickness
- Part dimensions
- Order quantity
- Expected annual volume
- Critical tolerances
- Surface requirements
- Formed features such as louvers or knockouts
- Deburring requirements
- Downstream bending and welding
- Coating or finishing requirements
- Prototype and production schedule
Without this information, quotations may compare different production scopes rather than the true cost of equivalent finished parts.
Conclusion: Which Process Should You Choose?
Choose CNC punching when the part contains repeated standard features, production volume is stable and available tooling can deliver a fast cycle time. It is especially valuable when cutting and forming features can be combined.
Choose laser cutting when designs are complex, quantities are lower, part variants are numerous or engineering changes are likely. Its flexibility and minimal tooling requirements can significantly reduce development cost and lead time.
For many projects, the correct answer is not determined by the process name but by the complete part geometry and production plan. To compare the available manufacturing routes, submit your drawings through Nova Fabrication’s request a quote page.